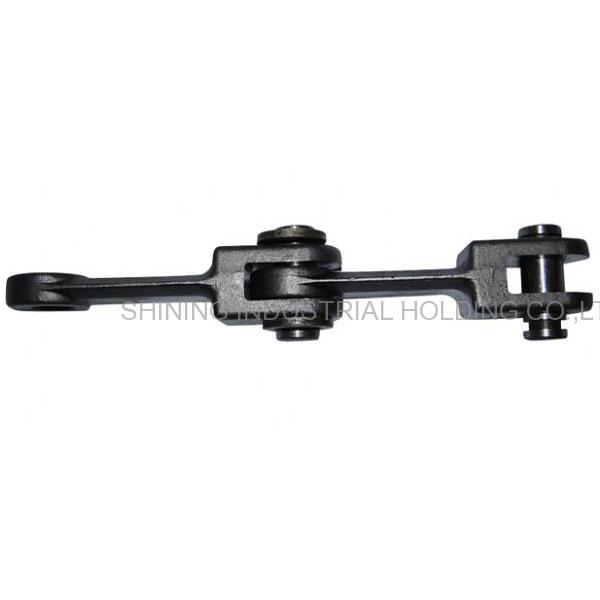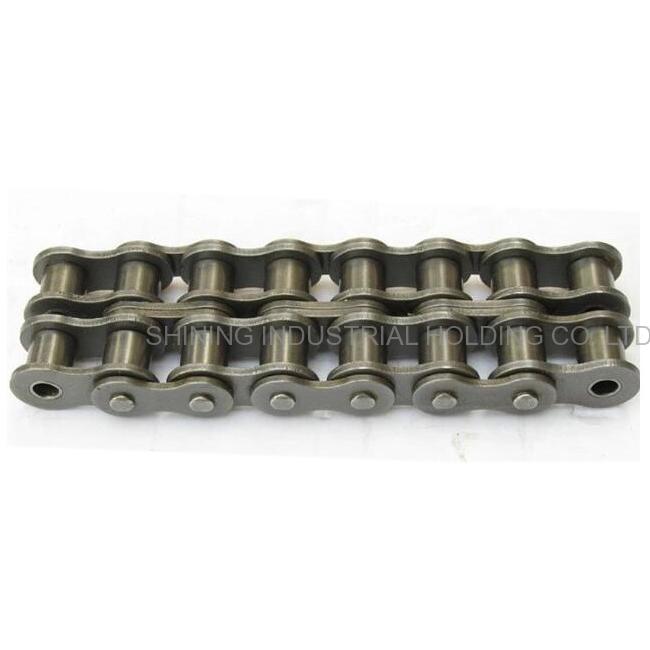


A sugar mill runs on chains. Intermediate carriers move mixed juice cake and bagasse between stations; feed and washing tables meter cane into the shredders; juice strainers and cush-cush elevators lift fibre-laden juice back into the process. Every one of these chains runs in wet, fibrous, abrasive, sugar-acid conditions that destroy an ordinary conveyor chain in a season.
SHINING has supplied sugar-mill chain for more than twenty years. This page explains the problems a mill actually faces, how SHINING's design and material choices answer them, which chain fits which station, and what stands behind the product. Detailed dimensional tables for every chain we make are on the individual product pages - this page is here to help you choose.
1. The Challenge in a Sugar Plant
A sugar mill is a corrosive, fibrous, high-throughput environment. The problems below are the ones mill engineers and procurement teams raise with us most often:
Bagasse and cane fibre wrap and jam the chain — Fibrous cane residue packs between plates, around pins and into attachments. A chain with tight clearances and unprotected joints will bind, jump the sprocket, or need constant cleaning - lost crushing time every shift.
Juice and sugar acid corrode the chain — The chain runs in juice, wash water and sugar-acid conditions. Untreated carbon-steel components rust, pit and seize at the pin and bush. Corrosion, not just wear, is what ends the life of a sugar-mill chain.
The chain stretches and the station timing drifts — Intermediate carriers and cush-cush elevators depend on chain pitch to keep station timing correct. As the pin and bush wear, pitch grows, the chain rides high on the sprocket and timing drifts - and the chain may snap.
A stoppage stops the whole crushing season — During crop, the mill runs flat out. A broken carrier or strainer chain stops the tandem, and the cost of lost crushing hours far exceeds the price of the chain itself.
Sprockets wear and eat new chain — A worn sprocket destroys a new chain quickly. If the tooth profile does not match the chain's actual pitch, or a large head sprocket cannot be re-rimmed in place, every chain change becomes a long shutdown.
Long lead times and hard-to-source spares — Mills often run equipment from many OEMs, sometimes decades old. Sourcing a correct spare chain or sprocket on a reasonable lead time is a real problem - the more so mid-season.
2. How SHINING Solves It
Material selection matched to the juice environment
Sugar-mill chain starts with the right steel. Wear parts (pin, bushing, roller) are engineered as a matched stainless set to eliminate galvanic corrosion. Pins, bushes and rollers are in 2Cr13 (SUS420J1), quench-hardened and tempered, or 17-4PH (1.4542 / AISI 630), precipitation-hardened in H1025/H1150 as specified, selected by juice duty - so the pin-and-bush joint resists both abrasive wear and sugar-acid attack that ends a carbon-steel chain. Sidebars are heat-treated alloy plate (40Cr / 42CrMo) for structural strength, or 304/316 stainless as specified.
Heat treatment - and IBR construction - as the core of wear life
The heat treatment is what sets service life. SHINING hardens, tempers, carburizes and induction-hardens in house. IBR chain has induction-hardened bushes and pins/rivets; WHX versions have through-hardened parts with induction-hardened pins/rivets as standard. The result is a chain that resists the pin-and-bush elongation a mill pays for, station after station.
Open, self-clearing geometry for fibrous cane
For feed and washing tables and for cane carriers, geometry matters as much as steel. SHINING supplies chains with the clearances and attachment forms that let bagasse and fibre clear instead of packing - reducing binding and cleaning downtime.
Forged rivetless chain for cane carriers
The 698HT / 678HT / 468HT / 998HT family is a drop-forged rivetless chain for feed tables and cane carriers. A forged link outlasts a fabricated one under the shock and abrasion of cane handling, and the rivetless joint is quick to connect and disconnect.
Cush-cush and juice-trainer chain built for the wet end
The juice strainer and cush-cush elevator chains - 4103 and WH9103HD - carry F-style attachments that hold the baskets through the juice train. Pins and bushes are hardened for the wet, fibrous, mildly acidic duty.
Chain and sprocket engineered as one system
SHINING cuts every sprocket to the actual pitch of the chain it will run, so tooth and chain wear together. Split (two-piece) sprockets bolt around the shaft for replacement without dismantling; segmental rims bolt onto a reusable hub so a large head or tail sprocket can be re-rimmed in place - a shift's work, not a shutdown.
3. Application Navigator
Mill station to chain family - use this to find the right page. Dimensional tables are on the linked product pages.
| Mill Station | Typical Chain / Sprocket | Why It Fits |
|---|---|---|
| Intermediate carriers (juice cake, bagasse) | 1131 (209 kN) / 09060 / 09061 / 09063 / 1796 / 2184 (450 kN) | The carrier family from light to the 2184 workhorse, in wet fibrous duty. |
| Heavy carriers | C84 (1,112 kN) / C69 (1,300 kN) | For the largest, heaviest carrier duty; K2 / A-type attachments to the mill's drawing. |
| Feed and washing tables | Welded steel chain WH78 (147 kN) to WH159 (950 kN), HD / XHD tiers | Welded construction with the strength tiers to match the table's load. |
| Cane carriers / feed tables | Forged rivetless chain 698HT / 678HT / 468HT / 998HT | Drop-forged links for shock and abrasion; rivetless joints for quick service. |
| Juice strainers / cush-cush elevators | 4103 (127 kN) / WH9103HD (267 kN), F-style attachments | F-attachments hold the baskets through the wet, fibrous juice train. |
| Every station above | Matched solid, split and segmental sprockets | Tooth-cut to the actual chain pitch; split and segmental for in-place replacement. |
Every chain above is quoted with its matched sprocket as one set. Where your mill runs a chain we have not listed - including older or non-standard stations - send the drawing or the OEM part number and we will quote against it.
Custom & Interchange Capability
Direct interchange — SHINING chain and sprockets are dimensioned to interchange with the major international sugar-chain brands, so they drop into an existing carrier or table without changing the drive or the take-up. Send the OEM part number or the original drawing and we will confirm the match.
Reverse-engineer from a sample — For obsolete or unbranded chain, send us a short length or a worn sample. We measure the pitch, plate and attachment geometry, agree the specification with you, and manufacture to it.
Build to your drawing — Non-standard pitches, special attachments, custom basket or carrier spacing, alternative materials and surface treatment - all available. Tell us the duty (load, speed, temperature, juice conditions) and we will propose the grade.
Sprockets to match any chain — We cut sprockets to the actual pitch of any chain, including other makers' chain already in your mill, in solid, split and segmental form, in steel or cast material.
Sample before season — For a new application we can supply a sample or trial length so your engineering team can prove the chain on the line before crop starts.
4. Built by SHINING
Sugar mills buy from SHINING because the product is engineered and made in one place, and because the numbers behind it can be checked. SHINING has manufactured chain since 2003 from a 36,000 m2 base in Changzhou, Jiangsu, China, with dedicated forging and link-chain plants and a full in-house heat-treatment and testing capability.
Quality is controlled at every step: incoming material is spectrograph-verified, key characteristics are inspected through production, and every order ships with inspection reports and a certificate of conformance. If the chain does not perform as specified, you have a manufacturer to go back to - not a trading desk.
| Area | What SHINING Provides |
|---|---|
| Manufacturing base | 36,000 m2 main production site in Changzhou, Jiangsu, China, with dedicated forging and link-chain plants. |
| In-house processes | Melting, forging, laser / flame / wire cutting, CNC turning, milling and grinding, robotic welding and shot blasting - all performed in-house. |
| Heavy capacity | Press capacity up to 400 MT; robot welding for hard-faced and scraper chains; automatic link-chain production lines. |
| Heat treatment | In-house hardening, tempering, case carburizing and induction hardening - the step that sets wear life. |
| Quality control | Every incoming material batch inspected; dimensional, heat-treatment and tensile / fracture inspection through production. |
| Testing lab | Tensile testing machine, hardness tester, roughness detector, spectrum analyser and chain-length measuring instrument. |
| Certification | ISO 9001:2015 and ISO 14001:2015; inspection reports and certificates of conformance issued with every order. |
| Worldwide supply | Exporting to cement, mining, steel, sugar, palm-oil, grain and material-handling plants across six continents. |
SHINING holds ISO 9001:2015 (cert. 46026Q00958R053) and ISO 14001:2015 (cert. 46026E00959R053) certification, issued by Shenzhen Huazhi (HZIC). Standard production lead time is 60 days.
Related Products
The 152.4 mm pitch workhorse of the carrier family, 450 kN average ultimate strength, with K2 / A-type attachments.
Feed and washing table welded chain from 147 kN to 950 kN, in standard, HD and XHD strength tiers.
307.19 mm pitch drop-forged rivetless chain for feed tables and cane carriers.
Solid, split and segmental sprockets, tooth-cut to the actual chain pitch - 09063, 2184, 1706, 6920 and more.