

9842 Clinker Apron Conveyor Chain: 250 mm pitch, OBR every 4 links, G4 every 2 links, 789 kN.
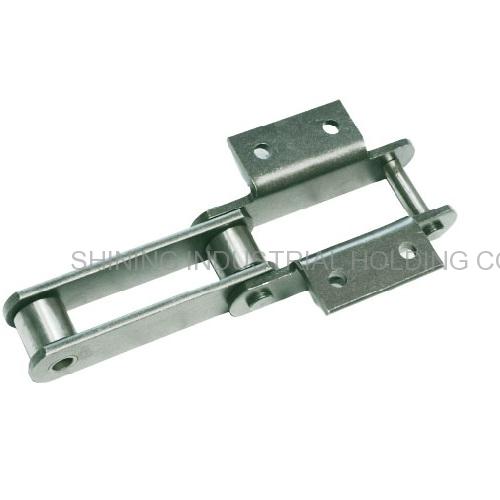
The SHINING 9842 is a Clinker Apron Conveyor Chain - a double-strand chain for clinker conveying on apron pan conveyors in cement plants. The G4 attachments, fitted every second link, fix the pans, and the out board rollers (OBR) every fourth link carry the pan conveyor along its tracks.
The chain runs on a 250 mm pitch with 95.25 mm chainplates, a 40 mm pin and a 140.2 mm OBR, and the average tensile strength is 789 kN. Every joint is fitted with a lube nipple for relubrication in service.
Clinker Conveying: pan conveyors carrying hot clinker from the cooler to the clinker store.
Continuous Hot Duty: hot, abrasive clinker handled around the clock.
Replacement Duty: built to interchange with the 9842 chain already running in the plant.
Two strands work in parallel and the G4 attachment on every second link gives a regular fixing point for the pans, so the pan line stays true along the full conveyor.
Each chainplate carries two holes: clinker fines spilled onto the chain fall straight through instead of packing into the joints and jamming the chain.
The plate openings sit clear of the load path, so the chain keeps its average tensile strength of 789 kN with the holes in place.
The out board rollers (OBR, also known as F-rollers) run outside the chain on a 140.2 mm rolling diameter: the OBR keeps the pan conveyor on its tracks instead of letting it wander off the rail.
Heat-treated working parts and heavy chainplates stand up to hot clinker and its abrasive fines, shift after shift.
A grease nipple on each pin lets maintenance teams relubricate the bearing in place, extending joint life on hot, abrasive duty.
The table below gives the 9842 Clinker Apron Conveyor Chain. Out board rollers are fitted every 4 links and G4 attachments every 2 links.
Material and heat treatment are selected for the duty. The chainplates are cut from quenched-and-tempered 40Cr alloy steel - the basis of the chain's 789 kN average tensile strength. The 42CrMo pins and 20CrMo bushes are further heat-treated, and the out board rollers are hardened on their running surfaces, so wear is taken at the hardened surfaces and the full service life of the chain is extended.

| Chain No. | Pitch (mm) | Chain plate height (mm) | Chain plate thickness (mm) | Inner width of inner chain plate (mm) | Pin dia (mm) | OBR dia (mm) | OBR spacing | Attachment | Tensile strength (kN) |
|---|---|---|---|---|---|---|---|---|---|
| 9842 | 250.0 | 95.25 | 12.0 | 66.3 | 40.0 | 140.2 | every 4 links | G4 every 2 links | 789 |
Matching sprockets are covered too: the 9842 segmental sprocket for this chain has its own page - see the 9842 Segmental Sprocket.
SHINING has manufactured conveyor chain and sprockets for cement plants for over twenty years, with drop forging, welding, machining and heat treatment under our own control. Every production batch is tensile-tested before shipment, and our quality system is certified to ISO 9001:2015 (46026Q00958R053) and ISO 14001:2015 (46026E00959R053).
We build to interchange. Send the OEM part number, an old link or a drawing, and we will confirm the match and reproduce it dimension-for-dimension, with sprockets and attachments cut to suit.
Standard production lead time is 60 days from receipt of the order and confirmation of the drawing. For breakdowns and planned shutdowns we can discuss an expedited slot - tell us your date and we will plan the delivery around it.
Our engineers support station and duty review, chain selection, wear and elongation analysis, maintenance planning, and genuine replacement parts. Send your conveying duty and we will size the chain for you.
Tell us your duty, your drawing or the OEM part number, and our engineers will come back with the right chain and a price. Email the sales team at sales@shiningco.com.